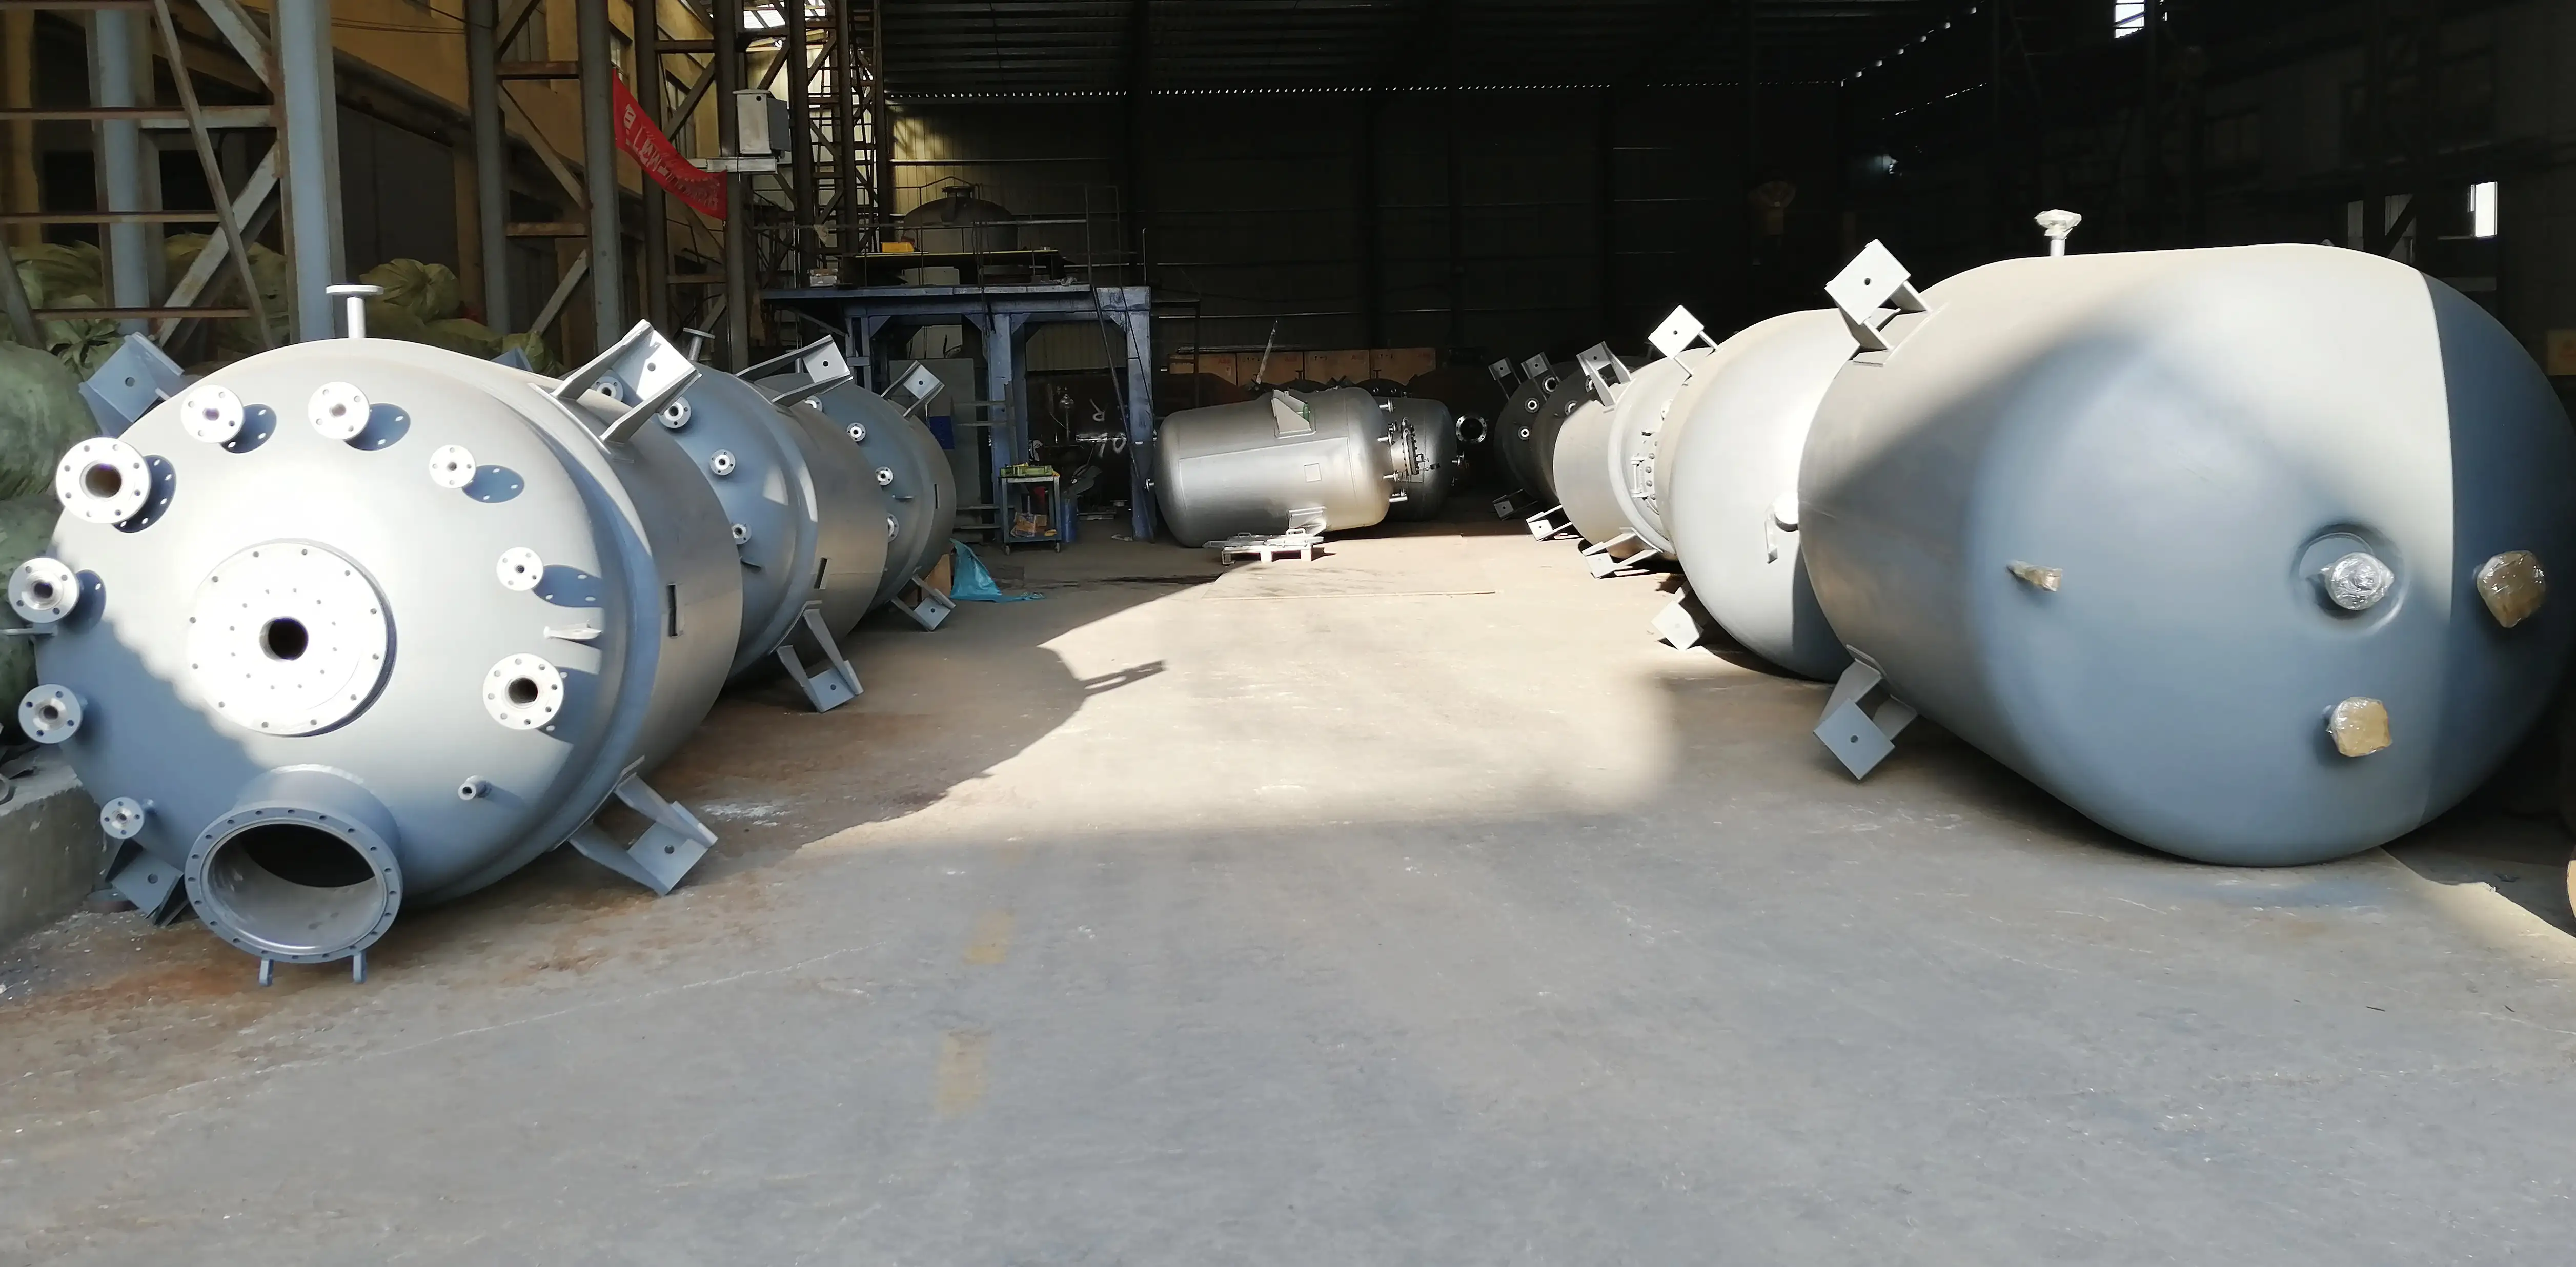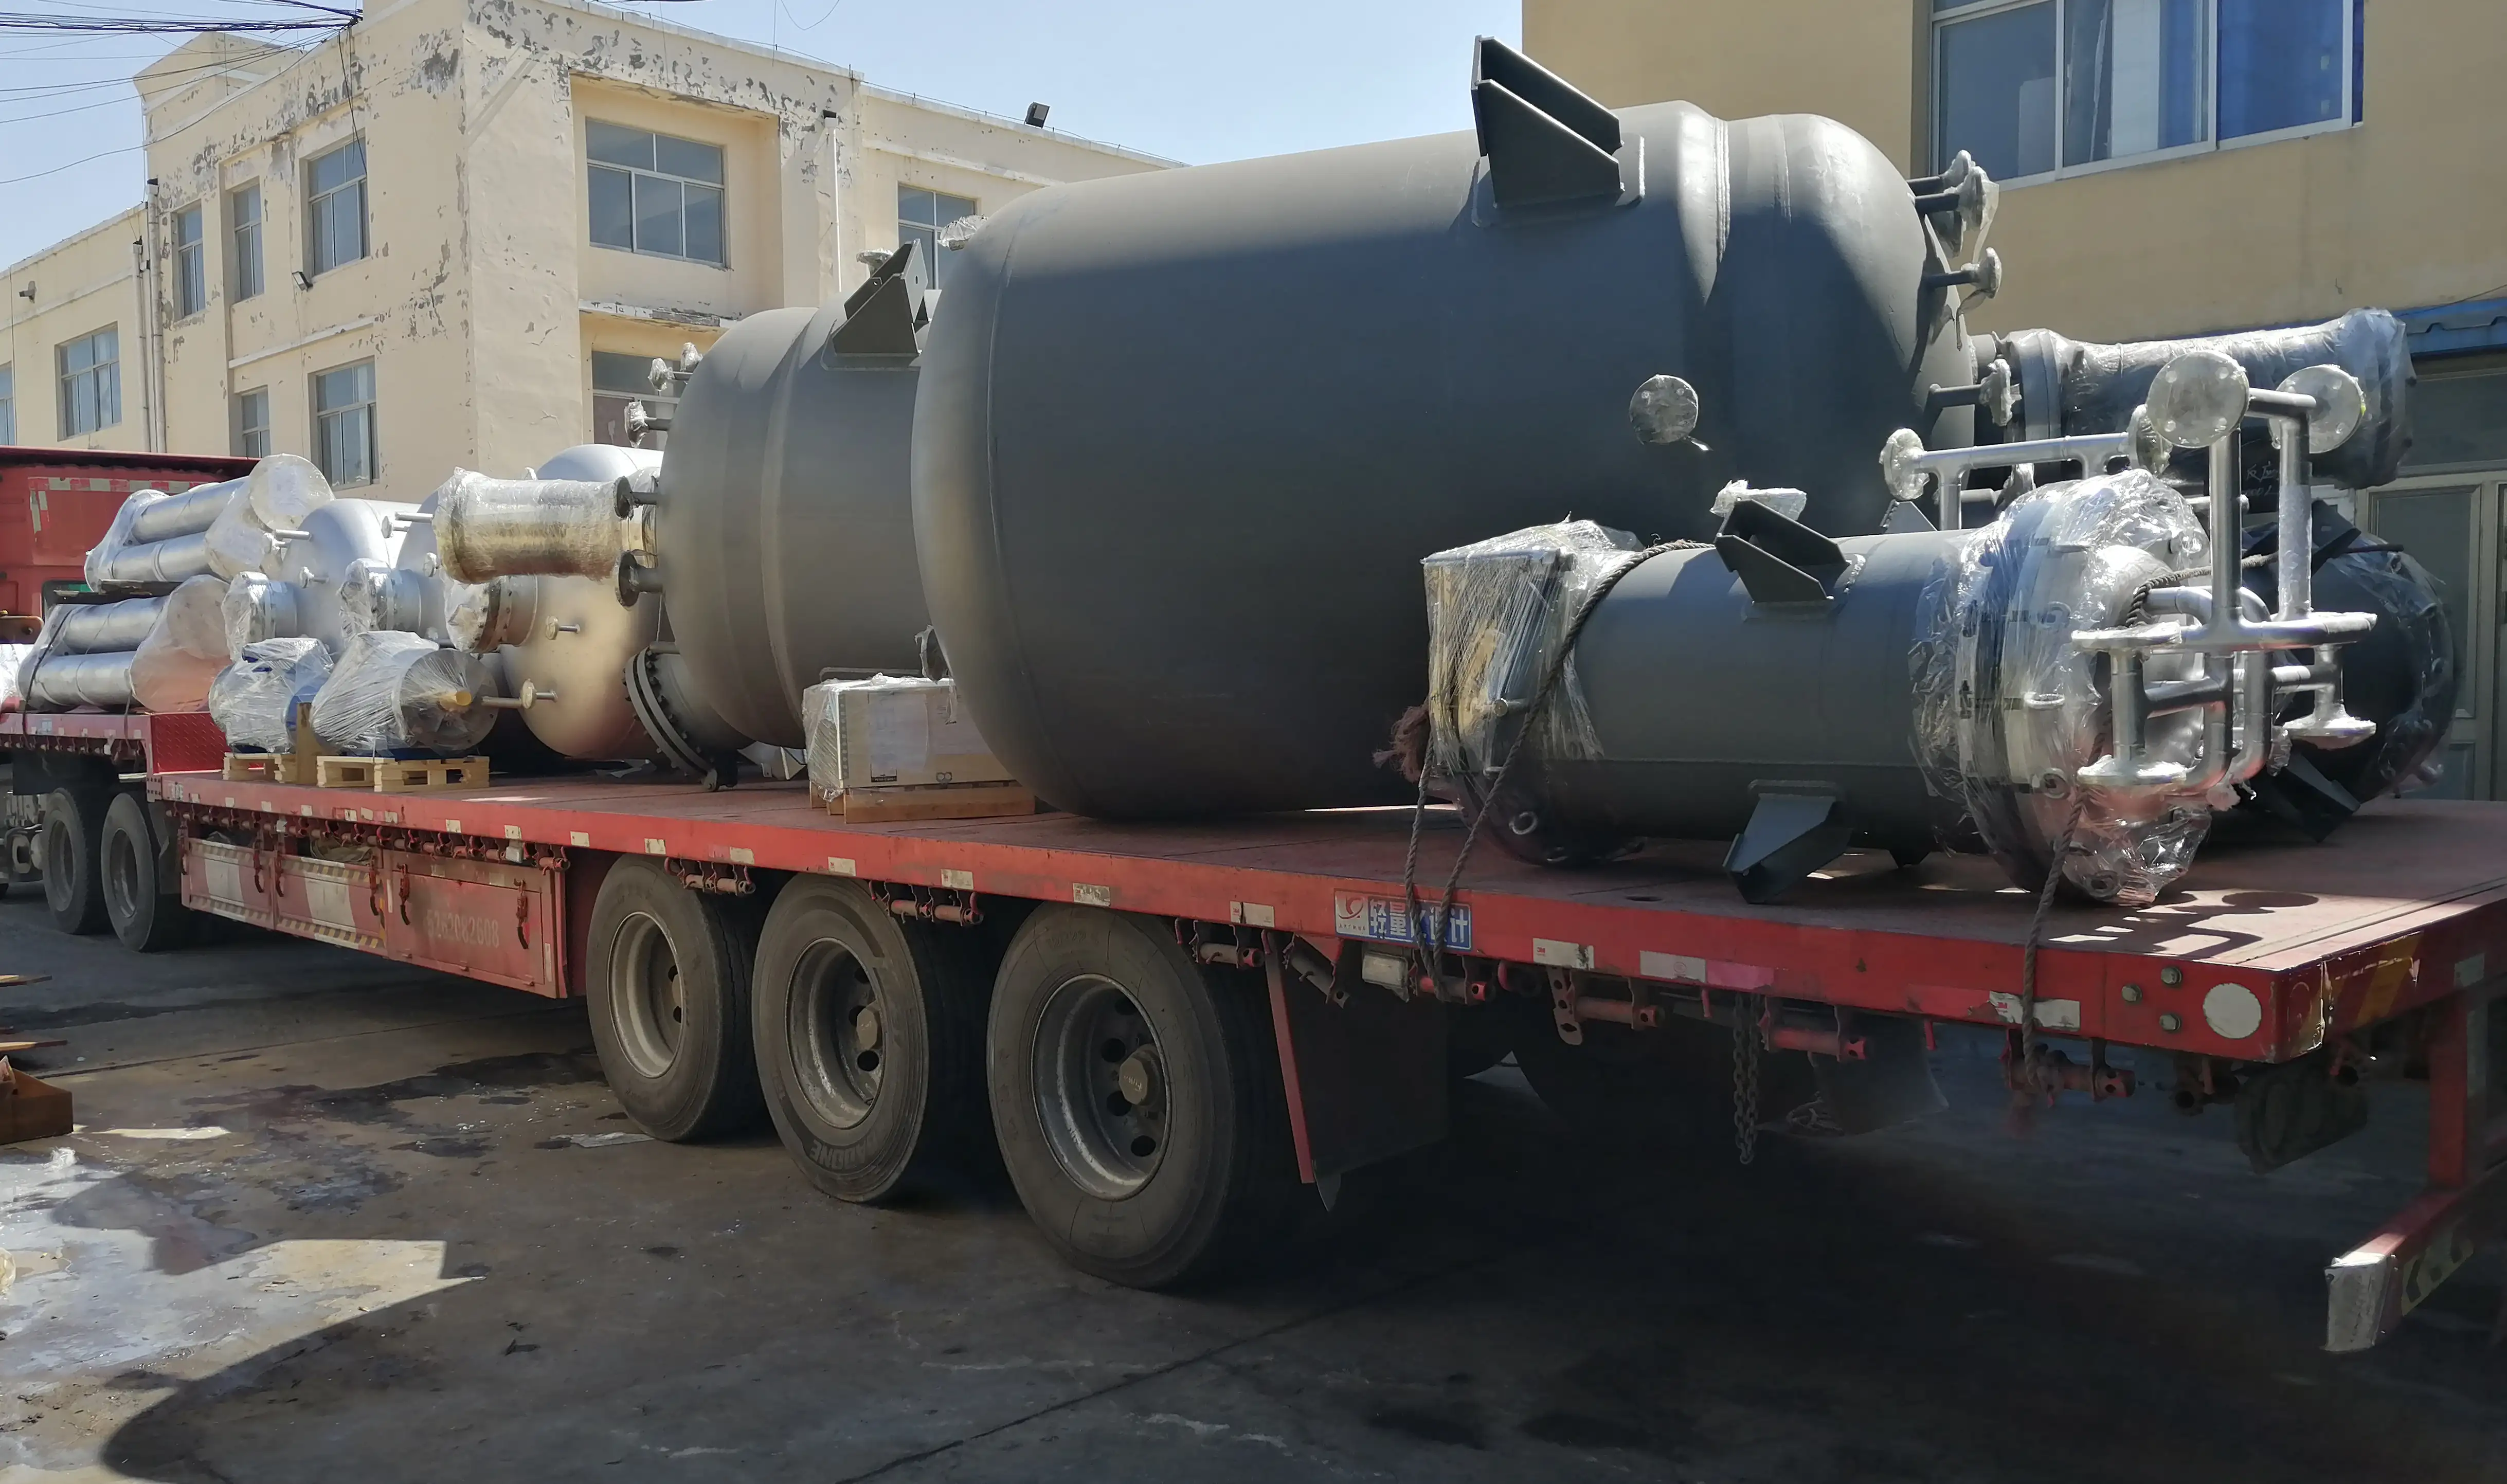
High-pressure hydrogenation systems up to 20 MPa with multi-layer cooling coils and explosion-proof configuration.
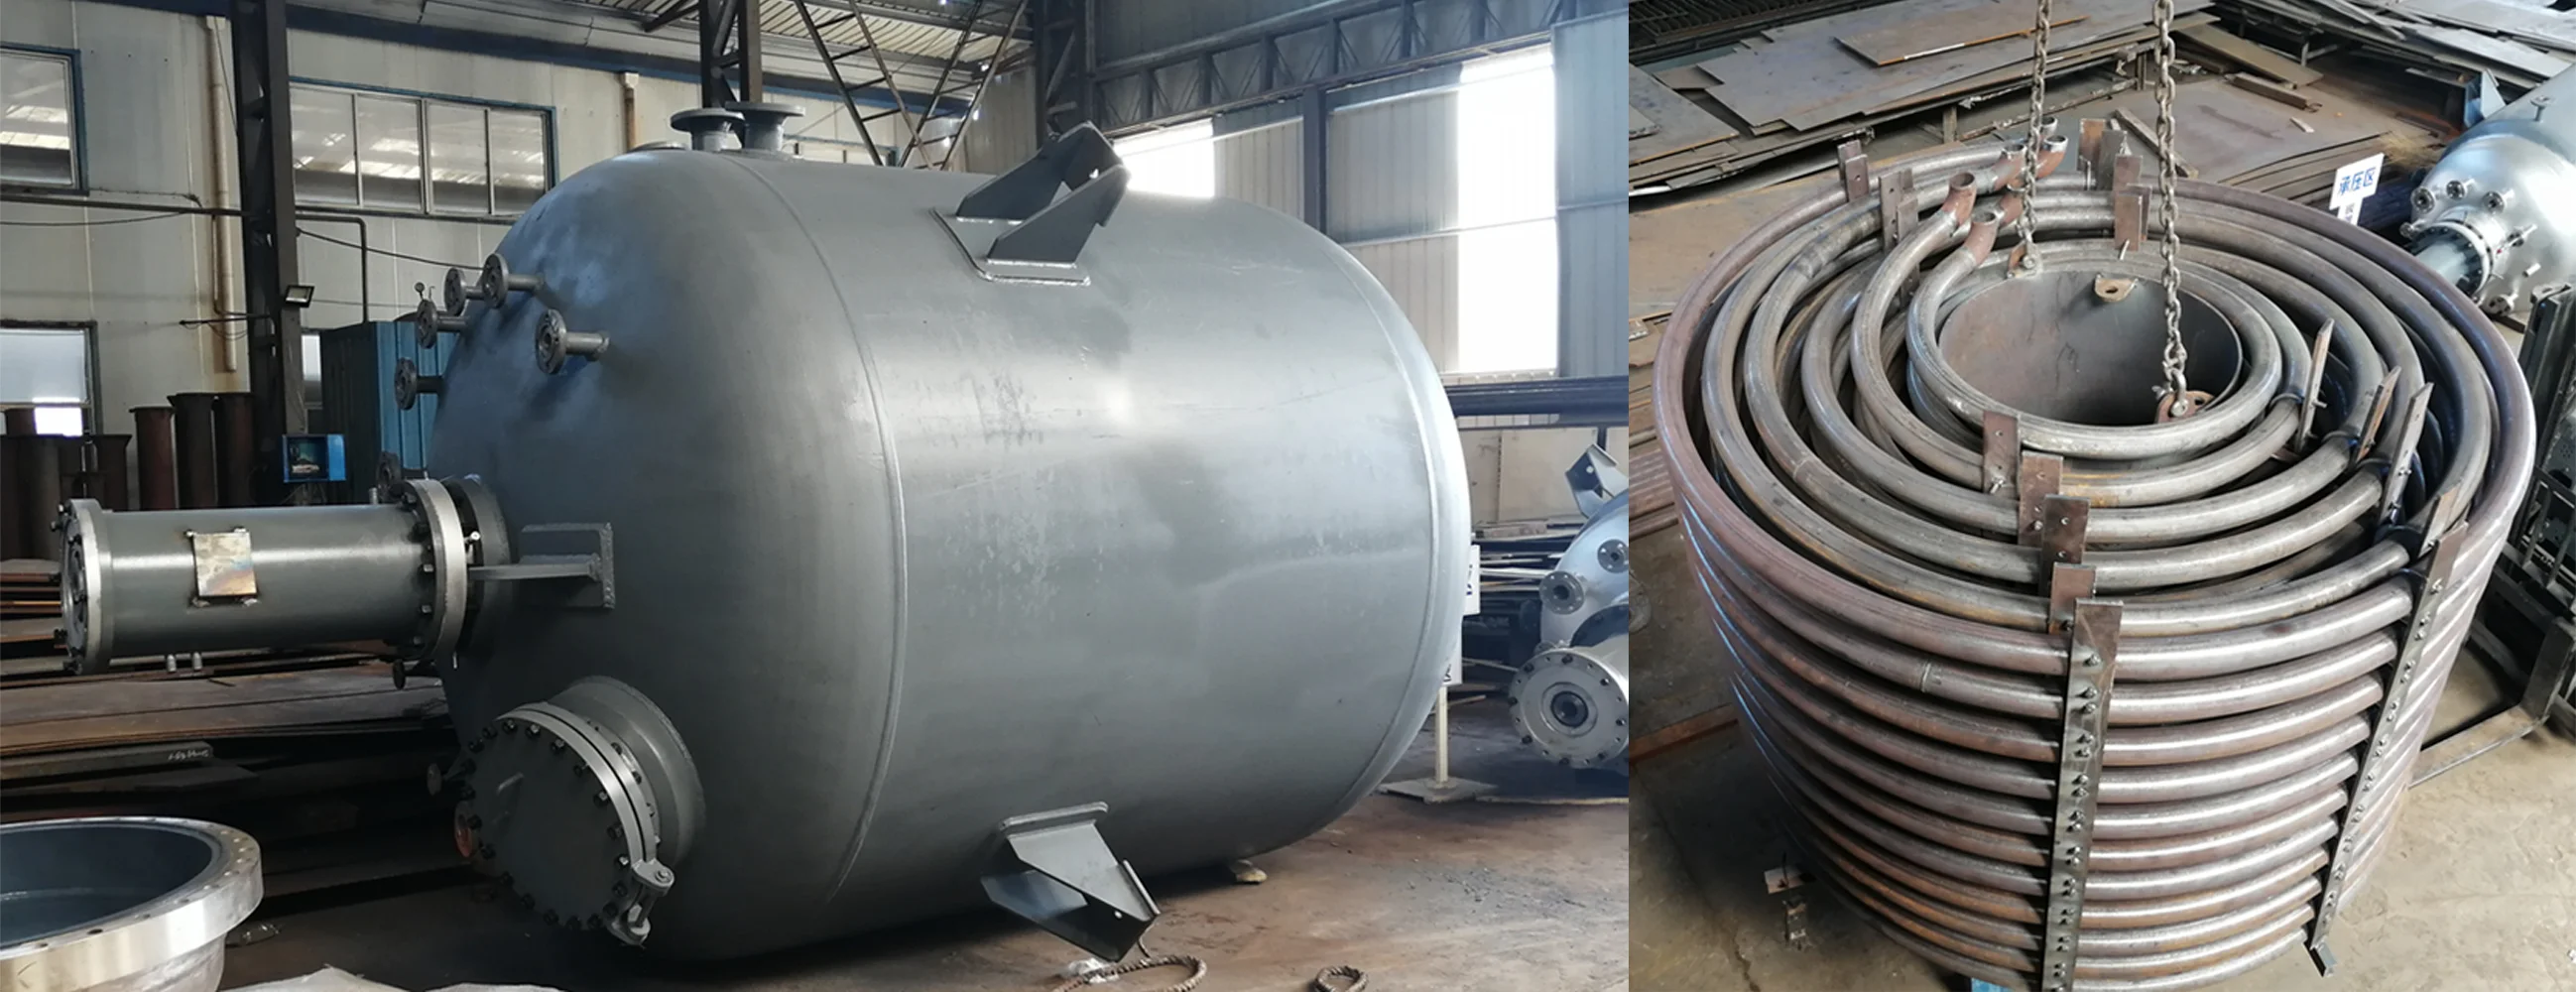
Hydrogenation is a chemical reaction where hydrogen interacts with other compounds, typically in the presence of a catalyst. This reduction process is fundamental to many industrial applications — from food additive production (sorbitol, xylitol, maltitol) to petrochemical refining and pharmaceutical synthesis.
Our hydrogenation reactors are specifically engineered for these challenging processes, handling the unique demands of high-pressure gas-liquid reactions with safety and precision.
Applications
Continuous and batch hydrogenation for producing sorbitol, xylitol, maltitol, and other sugar alcohols. Food-grade materials and strict purity control.
High-boiling liquid hydrogenation, hydrocracking of heavy oils, and selective hydrogenation processes. Handles difficult feedstocks with confidence.
Precise temperature and pressure control for sensitive pharmaceutical intermediates. Clean-in-place (CIP) compatible designs available.
Atmospheric gas-phase hydrogenation of benzene to cyclohexane — a classic continuous process our reactors handle efficiently.
High-pressure gas-phase hydrogenation of carbon monoxide to methanol synthesis. Tubular and tower reactor configurations available.
Edible oil hydrogenation, fat hardening, and specialty chemical production. Gentle processing preserves product quality.
Reactor Configurations
We offer both batch and continuous hydrogenation systems, configured for your specific feedstock and production requirements.
Ideal for high-boiling liquids or solids (dissolved or melted). Multiple agitation stages ensure thorough gas-liquid contact.
Trickle bed reactors or tubular reactors for continuous gas-liquid-solid three-phase flow. Higher throughput, consistent quality.
Specifications
| Parameter | Standard Range | Custom Options |
|---|---|---|
| Volume | 10L – 20,000L | Up to 50,000L available |
| Design Pressure | Up to 20 MPa | Higher pressures on request |
| Design Temperature | -20°C – 450°C | Custom temperature ranges |
| Agitator Speed | 20 – 400 RPM | Variable frequency drive |
| Coil Layers | 2 – 6 layers | Custom coil configurations |
| Material Options | 316L, 2205, Hastelloy C276 | Titanium, Monel, Inconel |
| Seal Type | Magnetic coupling (standard) | Dual mechanical seal available |
| Motor Rating | CT4 explosion-proof | Custom explosion-proof ratings |
| Standards | ASME VIII Div.1, GB150 | API, JIS on request |
Agitation Technology
Proper agitation is critical for hydrogenation efficiency. We design agitator systems optimized for your specific gas-liquid mass transfer requirements.
Standard configuration: paddle + self-priming + disc turbine disperser. Each layer serves a specific function in the hydrogenation process.
Our custom self-priming agitator includes a wind-catcher device that ensures hydrogen gas enters the impeller hollow shaft smoothly, maximizing gas-liquid contact.
Need something different? We design agitators for your specific medium viscosity, reaction kinetics, and heat transfer requirements. No off-the-shelf compromises.
Safety First
Hydrogenation involves high pressure and flammable gases. Every safety feature is designed to protect your operators and your facility.
Zero shaft leakage. No packing seals, no mechanical seals to wear out. Critical for preventing hydrogen leaks.
All electrical components are explosion-proof rated. Control box, motor, instruments — everything certified for hazardous areas.
Rapid heat removal prevents thermal runaway. Our coil design maximizes heat transfer area while maintaining structural integrity.
Material certificates, NDT reports, hydrostatic test reports, pressure vessel registration — everything you need for compliance.
Process Expertise
Intermittent hydrogenation for specialty chemicals, pharmaceuticals, and food additives
Trickle bed, tubular, and tower reactors for high-volume production
Systems rated up to 20 MPa for demanding hydrogenation applications
Efficient heat removal for highly exothermic hydrogenation processes
Hastelloy, titanium, and other exotic materials for aggressive processes
Sanitary finishes, clean-in-place capability, FDA-compliant materials
FAQ
Our hydrogenation reactors handle both liquid-phase and gas-phase hydrogenation. Common applications include benzene to cyclohexane, CO to methanol, edible oil hydrogenation, pharmaceutical intermediate synthesis, and sugar alcohol production (sorbitol, xylitol).
Hydrogen is small, flammable, and hard to detect. A leaking shaft seal isn't just inefficient — it's dangerous. Magnetic coupling seals eliminate the shaft penetration entirely, providing zero leakage. This is non-negotiable for hydrogen service.
Batch hydrogenation is better for smaller volumes, multiple products, and flexible operations. Continuous hydrogenation offers higher throughput and consistent quality for large-scale production. We design both types based on your production requirements.
Hydrogenation is highly exothermic. Our multi-layer internal cooling coil design provides maximum heat transfer area within the vessel. We calculate the exact cooling capacity needed for your specific reaction kinetics to prevent thermal runaway.
All our hydrogenation reactors come with CT4 explosion-proof motors and control boxes. Every electrical component is certified for hazardous areas. We also provide explosion relief devices, hydrogen detection systems, and interlock controls as part of the complete system.
Tell us your process conditions — volume, pressure, temperature, medium, catalyst — and we'll provide a technical review and detailed quotation within 48 hours.